


Copper Busbar Solutions for EV Fast Charging Piles: Current Carrying Capacity and Thermal Management
Aug 19, 2026
Leave a message
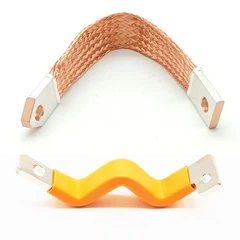
360kW+ EV fast charging systems require copper busbars engineered for continuous high-current transmission, low thermal rise, and long-term electrical reliability. A properly designed EV Charging Pile Busbar uses C1100 pure copper with 100% IACS conductivity, optimized cross-sectional area, controlled insulation thickness, and verified temperature performance under IEC and automotive reliability testing conditions.
For high-power charging infrastructure, the limiting factor is not only electrical conductivity but the combined control of Joule heat, contact resistance, insulation aging, mechanical stress, and environmental exposure. Heavy Duty Copper Busbar OEM solutions must integrate material selection, precision stamping, welding technology, and validation testing before mass production.

360kW+ EV Fast Charging Pile Requirements: High Current Copper Busbar Design Under Thermal Constraints
360kW DC Fast Charging Systems Require Busbars Designed for 500A-600A Continuous Current Loads
A 360kW charging pile operating at 600V DC requires approximately 600A continuous current. Compared with conventional AC charging systems, high-power DC charging introduces higher current density, faster temperature accumulation, and stricter requirements for conductor geometry.
The main engineering parameters include:
| Parameter | Engineering Requirement |
| System Power | > 360 kW DC Fast Charging |
| Operating Voltage | 400V-1000V DC |
| Continuous Current | 400A-600A |
| Peak Current | 800A+ depending on charging architecture |
| Copper Material | C1100 Pure Copper |
| Conductivity | ≥100% IACS |
| Dimensional Tolerance | ±0.01mm for precision stamping areas |
| Surface Treatment | Tin plating/nickel plating / anti-oxidation coating |
| Temperature Rise Control | According to IEC 61851 requirements |
The busbar cross-section directly determines current-carrying capability. Insufficient copper thickness causes excessive I²R losses, while oversized designs increase weight, cost, and assembly space.
Copper Busbar Cross-Section Calculation for EV Charging Applications
The basic current-carrying calculation follows:
P = I² × R
Where:
P = heat generation (W)
I = current (A)
R = electrical resistance (Ω)
Copper resistance is affected by:
conductor length
cross-sectional area
operating temperature
material purity
surface oxidation condition
For C1100 copper:
| Copper Busbar Thickness | Typical Continuous Current Range | Application |
| 3mm | 150A-250A | Low power charging modules |
| 5mm | 300A-400A | Standard DC charging systems |
| 8mm | 500A-700A | 360kW+ charging piles |
| 10mm+ | 700A+ | Ultra-fast charging platforms |
Thermal simulation is normally performed before tooling release. The target is maintaining a stable operating temperature under maximum charging current without exceeding insulation temperature ratings.
Request Free DFM Evaluation & Quote
Precision Manufacturing of Heavy Duty Copper Busbar OEM Components: Stamping, Welding and Inspection Control
IATF 16949 Manufacturing Process Control for EV Charging Busbars
High-current copper busbars require more than simple cutting and bending. Manufacturing accuracy affects contact resistance, thermal performance, and assembly consistency.
A qualified Fast Charging Busbar Manufacturer typically applies:
Progressive die stamping with ±0.01mm dimensional control
CNC bending for complex three-dimensional busbar structures
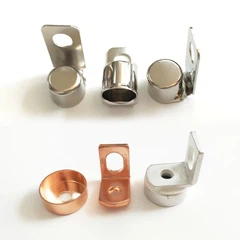
In-die riveting for integrated copper terminal assembly
Laser welding Cu-Cu and Cu-Al connection structures
CMM inspection for critical geometric dimensions
Surface roughness measurement before plating
Copper Material Selection: C1100 Pure Copper vs C2680 Brass
Different electrical connection points require different copper alloys.
| Material | Conductivity | Mechanical Strength | Typical Application |
| C1100 Pure Copper | ≥100% IACS | Medium | Main power busbar, battery connection |
| C1020 Oxygen-Free Copper | ≥101% IACS | Medium | High-reliability electrical joints |
| C2680 Brass | 25%-30% IACS | Higher | Terminal connectors, mechanical fixing parts |
C1100 copper remains the preferred material for EV charging busbars because electrical losses increase significantly when lower conductivity alloys are used in continuous high-current paths.
Welding Process Comparison for Copper Busbar Assembly
Copper welding presents challenges due to high thermal conductivity and reflective surface characteristics.
| Process | Advantages | Limitations | Application |
| Laser Welding Cu-Cu | Small heat-affected zone, high automation | Requires precise parameter control | Battery and charging modules |
| Laser Welding Cu-Al | Enables lightweight conductor transition | Requires oxide control | EV battery connection |
| Resistance Silver Brazing | Strong metallurgical bonding | Higher thermal input | Heavy current terminals |
| Molecular Diffusion Welding | Low contact resistance | Higher equipment investment | Premium electrical joints |
For mass production, welding parameters are monitored through:
welding energy monitoring
penetration depth inspection
cross-section metallography
electrical resistance testing

Epoxy Powder Coating vs Heat Shrink Tube Insulation: Selecting EV Charging Busbar Protection
UL 94 V-0 Insulation Performance Requirements for High Voltage Copper Busbars
Insulation failure can cause short circuits, arc discharge, and charging system shutdown. The insulation method must consider dielectric strength, mechanical protection, temperature resistance, and production consistency.
Two common solutions are epoxy powder coating and heat-shrink tube insulation.
| Comparison Item | Epoxy Powder Coating | Heat Shrink Tube |
| Dielectric Strength | >15kV/mm | 10-20kV/mm depending on material |
| Thickness Control | 0.2- 1.0 mm adjustable | Fixed thickness |
| Temperature Resistance | -40°C to 150°C | Typically -40°C to 125°C |
| Mechanical Protection | High adhesion coating | Flexible sleeve protection |
| Space Efficiency | Excellent | Requires additional clearance |
| Automation Capability | High | Medium |
| Typical Standard | UL 94 V-0 | UL 224 |
Epoxy Powder Coating Process Control
The epoxy powder coating process includes:
Surface cleaning and chemical treatment
Electrostatic powder spraying
Controlled curing process
Thickness measurement
Dielectric withstand testing
Key quality parameters:
coating thickness tolerance
adhesion strength
pinhole inspection
dielectric breakdown voltage
environmental resistance
For compact EV charging modules, epoxy coating provides better space utilization because it creates a uniform insulation layer directly on the copper conductor.
Environmental Reliability Testing: Salt Spray, Humidity and Long-Term Outdoor Operation
IEC and ISO Testing Requirements for Charging Infrastructure Components
EV charging piles are installed outdoors and exposed to:
humidity
temperature cycling
salt contamination
UV radiation
chemical pollutants
Copper busbars require corrosion-resistant surface treatment and validated environmental durability.
Typical qualification tests include:
| Test Item | Standard | Typical Requirement |
| Salt Spray Test | IEC 60068-2-11 | 96h-1000h depending on application |
| Temperature Cycling | IEC 60068-2-14 | Multiple thermal cycles |
| Humidity Test | IEC 60068-2-78 | High humidity exposure |
| Insulation Test | IEC 60664 | High voltage insulation coordination |
| Flame Rating | UL 94 | V-0 requirement |
Surface protection methods:
| Treatment | Function |
| Tin Plating | Improves solderability and oxidation resistance |
| Nickel Plating | High temperature corrosion resistance |
| Epoxy Coating | Electrical insulation protection |
| Anti-oxidation Treatment | Extends copper surface reliability |

Quality Assurance System for EV Charging Pile Busbar Manufacturing
PPAP Level 3 and CMM Inspection for Automotive-Grade Production
Automotive and charging infrastructure customers require documented process validation before production release.
Typical quality documents include:
PPAP Level 3 submission
Control Plan
Process Flow Diagram
PFMEA
Material certification
Dimensional inspection report
Welding validation report
Inspection equipment includes:
CMM coordinate measuring machine
Optical measurement system
Microhardness tester
Salt spray chamber
Burst pressure test equipment for cooling-related assemblies
A qualified Heavy Duty Copper Busbar OEM controls every production stage from copper material incoming inspection to final electrical performance testing.
FAQ: EV Fast Charging Copper Busbar Procurement
What is the typical PPAP Level 3 delivery time for EV charging busbar projects?
PPAP Level 3 delivery usually requires 4-8 weeks depending on tooling complexity, inspection requirements, and customer approval process.
How does a copper busbar manufacturer guarantee stamping die lifetime?
Progressive stamping dies are validated through trial production, dimensional capability analysis, and continuous monitoring to ensure stable tolerance performance.
Can manufacturers support small-volume EV charging busbar prototypes before mass production?
Yes. Engineering prototypes can be produced through CNC machining, laser cutting, and soft tooling before mass production tooling investment.
contact us

Send Inquiry