


Introduction to Silver Contact Recycling: A Must-Read for Industry Professionals Silver Contact Recycling Technology
Mar 03, 2026
Leave a message
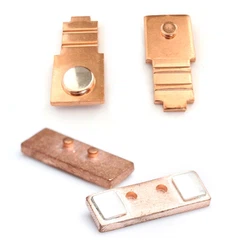
Silver contacts are widely used in various electrical equipment and are typical key functional components of electrical contacts. In systems such as electrical switches, relays, and circuit breakers, silver electrical contacts ensure stable current transmission and long-term reliable operation of equipment due to their excellent conductivity and corrosion resistance. With equipment upgrades, a large number of silver-containing components enter the scrap stage, including various types of contact materials such as Solid Silver Contacts and Silver Alloy Contacts. The standardized recycling of these silver-containing waste materials not only has significant economic value but also meets resource recycling and environmental compliance requirements, making it a fundamental technical path that industry practitioners must master.

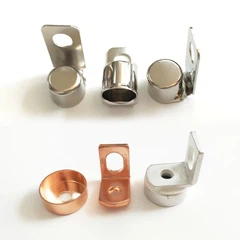
Silver contacts are typically fixed to the base metal by riveting or welding, such as Silver Alloy Rivets or Silver Solid Contact Rivets. To achieve effective separation of the contact from the base metal, high-temperature heating in a resistance furnace is required to decompose the adhesive layer or solder, separating the silver contact from the copper or steel base material. The core of this step lies in temperature control and separation efficiency management, ensuring contact integrity while avoiding silver oxidation and loss. For the recovery of Pure Silver Contacts and Alloy Silver Contacts, the quality of pretreatment separation directly determines the efficiency of subsequent leaching.
After physical separation, concentrated nitric acid is typically used as the leaching agent for wet treatment. Silver is oxidized in the nitric acid system to form a silver nitrate solution. The leaching temperature is controlled at 60–80°C, and the reaction time is approximately 2–4 hours. Excessive temperature accelerates nitric acid volatilization, while insufficient temperature affects the reaction rate. After leaching, the solution is clear and blue-green, and the solid residue is separated by vacuum filtration. This stage is suitable for the initial conversion and enrichment of silver from Silver Contact Points or other silver contact waste.
To further improve purity, the industry often uses solvent extraction for separation and purification. This method is based on the difference in the distribution of silver ions in different phases. The organic phase selectively complexes silver ions with impurity metals, achieving effective separation. The organic phase typically consists of an extractant, a co-solvent, and an inert organic solvent, such as triisooctylamine as the main extractant, combined with tert-butanol to improve dispersibility, and xylene as the solvent carrier. The pH of the aqueous phase is controlled between 0.5 and 2.
The two phases are mixed in a 1:1 ratio and brought into full contact under centrifugal shaking conditions, allowing silver ions to migrate from the aqueous phase to the organic phase. This step is highly effective in enriching silver ions in solid contact waste systems and is a core step in industrial purification.
After extraction, natural stratification is achieved using density differences, with the upper layer being a silver-rich organic phase and the lower layer being the aqueous phase. Strict interface control is required during separation to avoid cross-contamination. Subsequently, a silver salt solution is obtained through back-extraction or direct conversion and then proceeds to the electrolytic refining stage. Using direct current electrolysis at a potential of 0.2–0.5V, silver ions are reduced at the cathode to precipitate metallic silver, achieving a product purity of up to 99.99%. This process is applicable to various silver electrical contact waste systems, ensuring both recovery rate and purity while maintaining environmental control.
Overall, the key to silver contact recovery technology lies in three aspects: first, pretreatment separation efficiency; second, precise control of leaching and extraction parameters; and third, potential and impurity management during the electrolysis stage. By rationally selecting reagent concentrations, reaction temperatures, and time windows, a highly efficient and low-emission resource regeneration pathway can be achieved. With the increasing demand from power systems, new energy sources, and high-end electrical equipment, the standardized recycling and refining technology of silver-containing electrical contacts will become an indispensable and crucial link in the industrial chain.

- As a professional contact manufacturer, our Solid Silver Contacts, Silver Alloy Contacts, and related Silver electrical contacts are all manufactured using high-purity virgin silver materials. We do not use recycled silver as a raw material, ensuring stable and controllable conductivity and reliability. For high-quality contact product solutions, please contact us for detailed technical information.
contact us

Send Inquiry