


Does the hardness of pure iron determine the long-term reliability of a relay iron yoke bracket?
Jun 25, 2026
Leave a message
In the material selection system for power electronic metal components, the hardness parameter of pure iron directly determines the forming process and long-term operational stability. Relay system engineers often struggle with whether the hardness range of pure iron is suitable for their structural components. As a core magnetic bearing component of the relay, the Relay Iron Yoke Bracket has dual strict standards regarding the hardness and ductility of the base material. Industrial pure iron is uniformly defined as having a carbon content of less than 0.04%, and is divided into two categories: DT4 electric pure iron and YT series smelted pure iron. Annealed DT4 has a basic Brinell hardness ≤85, and its hardness increases slightly after cold rolling, but is far lower than that of ordinary low-carbon steel, making it a dedicated base material for electromagnetic structural components.

Impurity content is the core internal factor affecting the hardness of pure iron. Trace elements such as carbon, sulfur, and silicon can cause lattice distortion, simultaneously increasing the material's hardness and weakening its magnetic permeability. This can easily lead to hidden cracks when processing complex bending structures, directly affecting the dimensional stability of the Relay Steel Yoke under long-term on/off vibration conditions. High-end DT4C grade iron has strictly controlled total impurity content, maintaining a low-hardness, soft state, eliminating the risk of cracking during cold stamping and deep drawing. YT raw material, while pure iron, focuses on smelting requirements for impurity control, lacks electromagnetic performance standards, and is unsuitable for manufacturing structural components for various electromagnetic devices.
Cold and hot working processes alter the hardness range of pure iron. Annealing releases internal stress, uniformly softens the grains, and minimizes hardness, making it a standard pre-processing step for Relay Yoke Stampings. Cold rolling and cold drawing processes lead to work hardening, increasing the sheet hardness to HB90-110, suitable only for simple thin sheet cutting, and unsuitable for the multi-layer bending and countersinking required for relay yokes. Hot-rolled pure iron has dense grains and a hardness between annealed and cold-rolled materials, generally used only as raw material and not directly used for finished magnetic conductor brackets.
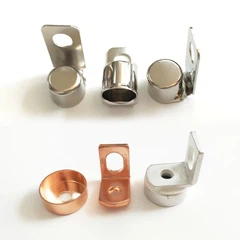
Annealed soft pure iron (HB≤85) offers optimal plasticity and deep drawing performance, suitable for stamping, laser cutting, and precision bending, making it the standard base material for manufacturing Sheet Metal Relay Yokes. This material exhibits no stress concentration at bending corners and will not warp or deform under long-term high and low temperature cycling. It also retains extremely low coercivity and high magnetic permeability, reducing relay coil operating losses. It is widely compatible with components such as magnetic yokes and armatures in new energy vehicle relays and industrial control switches. After forming, the entire machine can be assembled without secondary correction.
Cold-rolled hardened pure iron, with a hardness range of HB90~110, only supports simple punching and planar cutting. It cannot complete complex three-dimensional bending structures and is rarely used in the mass production of Magnetic Yokes. This type of material is only used for simple thin magnetic pads and small sensor monolithic iron cores. After forming thin sheets, the flatness is good, eliminating the need for a leveling process. However, the internal stress caused by cold working significantly weakens magnetic properties. Under frequent switching conditions, temperature rise and magnetic loss continuously increase, which does not meet the design standards for long-term reliable operation of relays.
In the new energy and industrial control power electronics industries, DT4A and DT4E annealed electric pure iron are preferred for the internal magnetic yoke supports of relays and contactors. This balances forming process and electromagnetic performance, ensuring dimensional stability of the Precision Relay Yoke Stamping Part in alternating environments ranging from -40℃ to 125℃. This grade of pure iron has low residual stress after stamping, and when assembled with copper conductive stamped parts, the entire unit exhibits no structural deformation after millions of on/off vibration tests, making it the most versatile material choice for low-voltage electrical electromagnetic structural components.
Three common misconceptions exist in material selection within the industry: First, the belief that pure iron's low hardness prevents it from bearing mechanical stress. Magnetic Yoke Metal Stamping for EV Relay only serve a magnetic conduction function and do not bear loads; for stress reinforcement, they can be combined with carbon steel supports. Second, the misconception that higher hardness equates to better magnetic properties. Cold work hardening damages the grain structure, and electromagnetic devices must use annealed soft-state pure iron. Third, the confusion between raw material pure iron and electric pure iron. Their performance indicators differ significantly and they are not interchangeable for relay core processing.
The overall selection logic can be summarized into three application scenarios: For manufacturing magnetic conductive structural components for relays and solenoid valves, annealed DT4 series low-hardness electrical pure iron is selected to ensure the forming accuracy and magnetic properties of the Sheet Metal Relay Yoke Assembly; for use only as a raw material for smelting and melting, YT series pure iron is selected, where hardness is not a consideration; and for simple, non-bending thin magnetic conductive sheets, cold-rolled pure iron can be used in small quantities. Pure iron cannot have its hardness increased by quenching. If the structure requires high strength, a composite structure design using dissimilar metals must be adopted to avoid the insufficient strength of pure iron alone.

Based on the aforementioned pure iron material selection and forming process standards, we have standardized the mass production of a full range of Relay Iron Yoke Brackets. The entire process utilizes DT4 annealed electric pure iron as the base material, employing integrated processing including progressive die stamping, stress-relief leveling, and precision cutting. We strictly control material hardness, magnetic permeability parameters, and dimensional tolerances, making our products suitable for assembly needs across all categories of relays in automotive, photovoltaic, and industrial control applications. All batch deliveries come with complete material testing and performance verification reports, mitigating common engineering problems such as magnetic loss, deformation, and engagement failure from the outset.
For project specifications matching, material performance test reports, and Electrician Pure Iron Strip Stamped sample verification solutions, please send your relay drawings and operating parameters for consultation and discussion.
contact us

Send Inquiry