


Can brazing meet the long-term usage requirements of Electrical Contact Assembly with Silver Welded Tip?
Jun 23, 2026
Leave a message
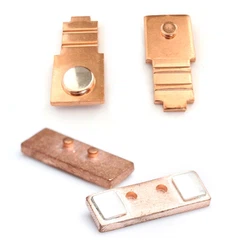
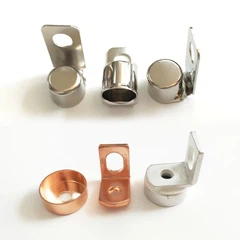
Brazing relies on a filler metal with a melting point lower than the base metal to join dissimilar metals. The operating temperature is controlled below the melting point of the base metal. The liquid filler metal wets the base metal, fills the gaps, and causes interfacial diffusion. After cooling, a stable joint is formed. This process is commonly used to bond the silver contacts to the copper substrate in Electrical Contact Assembly with Silver Welded Tip. Compared to fusion welding, brazing has a lower overall heating temperature, less workpiece deformation, and controllable dimensional accuracy. It is compatible with both silver and copper, two dissimilar materials with excellent thermal conductivity, and has no strict limitations on substrate thickness differences, making it suitable for batch processing of various small conductive contacts.

Brazing offers efficiency advantages for batch processing. Multi-specification Silver Contact Welded Assembly for Contactor can be heated synchronously to complete multiple welds at once, significantly reducing the processing time per piece. The supporting production equipment has a simple structure and low initial production line investment costs, making it suitable for small to medium-scale component production. This process produces a smooth, flat joint surface with excellent airtightness. The metallographic structure of the base material remains largely unchanged, preserving the wear-resistant and conductive properties of the silver contacts and the high thermal conductivity of the copper substrate. This makes it perfectly suited to the production standards of precision conductive components in instruments, relays, and smart meters.
The brazing process used for manufacturing silver-copper contacts has obvious performance shortcomings. In the long-term current-carrying and cold-hot cycling conditions, the brazed joint strength and heat resistance of the Brazing Silver Electrical Contacts have inherent limitations. The mechanical properties of the brazing filler metal are weaker than those of the silver-copper base material. The mechanical properties of the solder itself are weaker than those of the silver-copper base material. The industry generally adopts a longer lap joint structure to enhance the load-bearing capacity. At the same time, the standard for cleaning the surface of the workpiece before welding is very strict. Oxide layers and oil stains will directly weaken the wetting effect of the solder, resulting in false welding and porosity defects. The procurement cost of special silver-based solder is relatively high, and long-term large-scale production will continuously increase the overall manufacturing cost of the component.
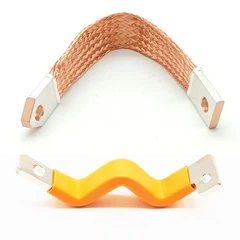
The complete brazing forming process has standardised operation logic. Before processing the Copper Bar Silver Contact Attachment, the silver contacts and the copper base contact surfaces need to be thoroughly cleaned. An overlapping structure is used for assembly, and the brazing filler is arranged around the weld gap. The workpiece is heated to the melting temperature of the brazing filler, and the liquid brazing filler spreads over the joint by capillary action. The silver and the copper base material, as well as the brazing filler, mutually dissolve and penetrate, generating an alloy transition layer at the interface. After natural cooling and solidification, a conductive joint is formed. The entire process is highly sensitive to temperature, gap, and cleanliness. Any deviation in any parameter will cause abnormal contact resistance at the contact points.
From an industry application perspective, brazing is not suitable for heavy-duty, dynamic, impact-sensitive high-power electrical components. Precision Welding for Copper Part is primarily used in low-voltage instruments, small relays, single-phase smart meters, and low-voltage signal switches. Brazed joints offer dimensional stability and uniform conductivity, enabling connections between metals and some non-metallic materials. It is widely used in thin-plate sandwich structures, honeycomb conductive structures, and precision wire connector processing. However, for equipment operating under prolonged high-temperature conditions, such as high-current contactors in new energy applications and industrial circuit breakers, brazed joints are prone to creep and interface cracking, making it difficult to meet the requirements for stable service for more than ten years.

Considering the advantages and disadvantages of brazing, it is clear that traditional brazing solutions struggle to simultaneously meet the three core requirements of silver contact components: long-term high-temperature resistance, high mechanical strength, and batch consistency. Our factory has independently developed and mass-produced Welded Ag Contact Assemblies, optimising the welding process to replace traditional brazing. This eliminates insufficient heat resistance and interface drift defects caused by brazing filler metal, resulting in welds free of impurities and inclusions, no cracking under high and low temperature cycling, and long-term stable contact resistance. It is suitable for use in meters, energy storage, and low-voltage relays across all scenarios, and a complete welding performance test report is provided for each batch.
If you are currently selecting and verifying the reliability of contact components for low-voltage electrical appliances and smart meters, please feel free to contact our engineering team to request samples, process data, and batch quotations for Electrical Contact Assembly with Silver Welded Tip, and to discuss long-term supply cooperation.
contact us

Send Inquiry