



Outer Cap And Automotive Fuse Terminals
Products Description
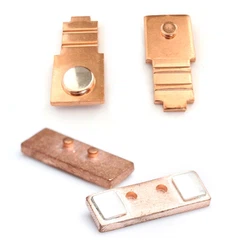
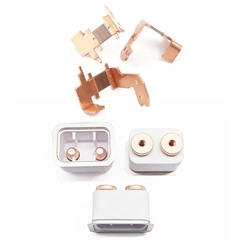
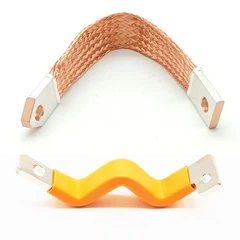
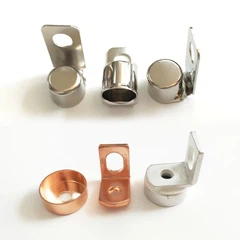
The Outer Cap and Automotive Fuse Terminals, primarily composed of a fuse terminal and an outer cap, are a crucial interface unit between the fuse and external circuitry. Its core functions extend beyond current transmission; it also ensures:
Stable, low-resistance electrical connection
Suppressing temperature rise and localized overheating
Improving the fuse's mechanical and environmental adaptability under complex operating conditions
Ensuring safe isolation of the vehicle or system in fault conditions
This product series is specifically designed for new energy platforms and is suitable for applications involving high current, high vibration, high temperature differences, and high-frequency assembly.

Key Details: Automotive-Grade Quality Showcased in Precision
Terminal Contacts
Features an arc-shaped raised contact design, increasing the contact area (30% larger than flat contacts) while reducing insertion and removal resistance, preventing fuse contact wear, and extending service life.
Contact Cap Sealing
An internal annular sealing groove and matching silicone ring achieve IP67 protection, effectively isolating internal electrolyte vapor from external moisture and preventing Copper End Cap and Fuse Terminal Contact oxidation.
Installation Guidance
The top of the Copper Metal End Cap and Fuse Link Contact features a double-sloped guide design, automatically calibrating when the insertion deviation is ≤2mm, adapting to high-speed assembly on automated production lines and reducing assembly defect rates.
Packaging Protection
Packaged in an anti-static bag + blister tray + moisture-proof carton, each product is individually sealed (including desiccant), and the Copper Cap and Fuse End Blade Femules area is covered with a protective sleeve to prevent plating scratches and contact cap deformation during transportation.

Manufacturing Advantages and Technological Features: Precision Craftsmanship Creates Superior Quality
Our manufacturing advantages lie in the deep integration of advanced processes and automated testing, ensuring that every Cap and Contact for Battery Power and Auxiliary Fuses meets automotive-grade quality standards.
High-Precision Stamping and Cold Forging: Utilising high-speed precision stamping presses and progressive dies, we ensure that the contact blade's contour and hole dimensions achieve an accuracy of ±0.02mm. Critical contact areas employ cold forging, using high-pressure extrusion to make the metal grains denser and significantly improve surface finish, laying the physical foundation for low contact resistance and excellent conductivity.
Automated Riveting/Injection Moulding Assembly: On a fully automated workstation, the assembly process of the contact blade and cap is completed by robots. Riveting pressure, time, and other parameters are precisely controlled and monitored in real time by a program, ensuring that the crimping torque at each connection point is completely consistent, resulting in a bonding strength far exceeding that of manual assembly.
Surface Treatment Process: To further enhance conductivity and oxidation resistance, the contact blade surface undergoes a precision electroplating treatment. We offer both tin plating and silver plating options. Silver plating offers lower resistivity and superior resistance to sulfidation than tin, making it the preferred choice for high-end applications demanding ultimate performance.
End-to-end traceability and rigorous testing: Each component has a unique QR code, allowing traceability of its raw materials, production equipment, operators, and key process parameters. We regularly conduct insertion/extraction force tests, contact resistance tests, temperature rise current tests, vibration tests, and salt spray tests to ensure superior Cap and Contact for Battery Pack Fuse performance under simulated real-world conditions.

Detailed Demonstration: Microscopic Evidence Defining Superior Quality
Microscopic Texture of the Contact Beam Surface
Under an electron microscope, the silver plating layer is dense and uniform, free of pores or cracks, and tightly bonded to the base copper alloy. This is fundamental to achieving low-resistance, long-life contact.
01
Metallographic Structure of the Weld Interface
Metallographic photographs of the weld cross-section after laser welding show uniform weld penetration, fine grains, and no defects such as porosity or slag inclusions, proving that the joint interface has conductivity and mechanical strength comparable to the base material for Cap and Contact for Hybrid Electric Vehicle Fuses.
02
Microstructure at the Forming Bending Point
Observation of the bending radius (R-angle) of the key elastic beam reveals continuous and complete material flow lines, without microcracks or significant thickness reduction, demonstrating precise control of the forming process and full utilisation of material ductility.
03
Permanence and Traceability of Product Identification
Laser-marked batch numbers, material codes, and other information are clear, wear-resistant, and high-temperature resistant, supporting quality traceability throughout the entire Cap and Contact for Fast Acting EV Fuse lifecycle.
04

contact us

Hot Tags: outer cap and automotive fuse terminals, China outer cap and automotive fuse terminals manufacturers, suppliers, factory, Welding Joints For Fuse, Fuse Cap and Contact, Copper Cap Contact For Vehicle Fuse, Copper Cap Contact For Electric Cars, fuse contact and cap, Outer Cap and Contact
You Might Also Like


Send Inquiry