


How to control the quality of copper processing and achieve stable and efficient Progressive Die Stamping Service with Copper Parts?
Jul 10, 2026
Leave a message
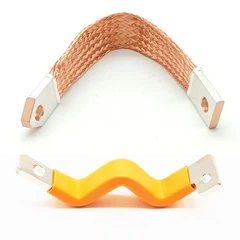
In the field of precision metal forming, Progressive Die Stamping Service with Copper Parts is the mainstream process for batch processing of copper and brass sheets and strips. The inherent plasticity, oxidation characteristics, and alloy composition of copper directly affect the parameter settings of the entire stamping process. Copper is soft and highly ductile; in the hot rolling stage, low-temperature, high-rate rolling is preferred to reduce high-temperature oxidation, while the single-pass cold working limit is higher in the cold rolling stage. Brass, on the other hand, is categorized by its zinc content, with high-zinc alloys prone to forming brittle phases at high temperatures. Therefore, the initial ingot heating and hot rolling temperature control need to be managed separately to lay a qualified base material foundation for subsequent continuous progressive stamping.

Ingot heat treatment is a crucial preliminary process to ensure the stability of the finished product in the Bending Laser Cutting Stamping Copper. The heating atmosphere standards for the two types of copper are completely different. Copper ingots are prone to oxidation upon heating. Oxygen-free copper requires a slightly reducing atmosphere, while oxygen-containing copper is only suitable for neutral furnaces maintained under positive pressure. Segmented heating and low-temperature unloading throughout the process avoid oxygen infiltration and hydrogen poisoning. Brass often uses a slightly oxidizing furnace atmosphere. High-zinc brass is strictly prohibited from high-temperature heating to prevent dezincification defects. Complex brass requires pre-releasing casting stress to prevent the continued expansion of inherent cracks in the strip during progressive stamping.
The cold rolling process parameters of the base material directly determine the continuous production stability of Copper Stamped Pressing Cutting Assembly Parts. Copper has significant advantages in plasticity, allowing for a very high cold working rate between two annealing cycles. Conventional batch stamping does not require intermediate annealing. Brass varieties are clearly differentiated. Low-zinc simple brasses, such as H90 and H96, can achieve a single-pass processing rate of over 75%, while complex alloys such as leaded brass have low plasticity, with a single-pass processing rate of less than 50%. Process design must allow for machining allowances to prevent edge cracking, strip breakage, and downtime during high-speed progressive stamping.
Annealing is a crucial step in eliminating stamping hardening and internal stress in copper. Annealing furnaces used in Progressive Die Stamped Copper Parts for MCCB require a protective atmosphere. Pure copper is highly susceptible to oxidation during annealing, necessitating complete isolation from air protection throughout the process. Stress-sensitive brasses such as H62 and HPb59-1 must undergo stress-relief annealing within 24 hours of cold working to prevent warping and cracking during storage. The lower limit of the annealing temperature range is selected for high-zinc brass to prevent high-temperature dezincification, which can cause surface pitting on stamped parts, and ensure the appearance quality after progressive stamping.
Surface treatment and finishing processes address the shortcomings in finished product protection in the Pressed Copper Stamping Sheet. Copper parts are highly prone to oxidation and discoloration after stamping; pure copper requires timely cleaning and passivation. Lining paper is used throughout the processing to prevent scratches from soft sheet metal, and precise control of tool pressure at the shearing station eliminates indentations. Brass pickling requires strict control of the pickling solution concentration and immersion time to avoid excessive zinc removal. High-zinc, hard-state stamped parts should not be repeatedly straightened; after multiple shaping processes, stress-relieving annealing should be applied to stabilize the dimensional accuracy of the copper parts.
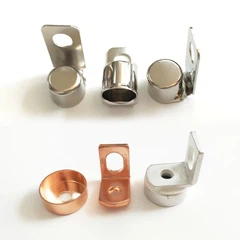
Environmental and substrate micro-control can significantly improve the yield rate of Electrical Contact Copper Metal Stamping Terminal. Copper is sensitive to temperature, humidity, and dust. In high-humidity environments, copper rapidly forms an oxide film, which can disrupt the continuous stamping effect of progressive dies. Simultaneously, even slight fluctuations in the phosphorus and zinc content of copper can alter recrystallization characteristics. Long-term, high-volume stamping necessitates the establishment of material testing standards, fine-tuning of die clearance and stamping speed according to copper batches, balancing forming quality and die wear, and achieving efficient and stable continuous progressive stamping production of copper parts.

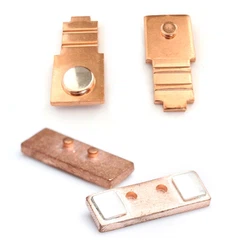
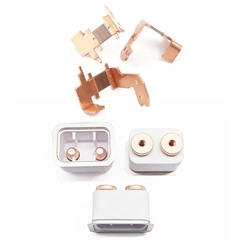
Leveraging our comprehensive and mature copper processing management system, we offer standardized and customized Progressive Die Stamping Service with Copper Parts. This service is suitable for mass production of copper and various brass sheets, balancing precision dimensional control, surface protection, and high production efficiency. We adjust the stamping, annealing, and passivation processes according to different working conditions, such as conductivity and load-bearing requirements, effectively addressing common production defects in copper stamping, such as cracking, oxidation, and dezincification, ensuring a stable delivery of high-yield copper stamped parts. We welcome your product drawings and bulk order requests for consultation and discussion to quickly finalize your customized stamping processing solution.
contact us

Send Inquiry