



Welded Electrical Contact Parts
Products Description

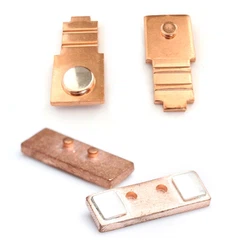
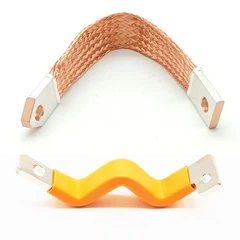
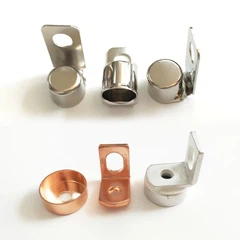
Welded Electrical Contact Parts refer to conductive components firmly welded to a metal substrate using silver-based alloys, copper-based materials, or composite contact materials through methods such as cold welding, projection welding, spot welding, and brazing. Their core value lies in:
Stable conductivity: Ensuring reliable closure and long-term continuity of electrical circuits.
Excellent arc resistance: Reducing erosion and extending service life.
Strong bond strength: Uniform weld joints and stable interface structure.
Low contact resistance: Improving system efficiency and reducing heat generation.
High-frequency switching capability: Adapting to high-speed operation scenarios.
These characteristics make them particularly suitable for equipment and systems with extremely high electrical reliability requirements.
Core Technical Features: Breaking Through the Performance Limitations of Traditional Welding
Low Heat Deformation Welding Technology
Utilizing low heat input processes such as "laser precision spot welding" and "resistance spot welding," the weld heat-affected zone (HAZ) width is ≤0.5mm, and the overall deformation of the part is ≤0.02mm, far superior to traditional arc welding (deformation ≥0.1mm).
Weld Conductivity Optimization
Through weld composition control (adding conductive alloying elements) and post-weld densification treatment, the Silver Brazed Electrical Contacts resistance is ≤3mΩ, and the difference between the weld and the contact body resistance is ≤5%, preventing the weld from becoming a conductivity bottleneck.
Complex Structure Welding Simulation
Using finite element simulation to simulate the welding process, the weld position, welding sequence, and energy parameters are optimized to ensure dimensional accuracy and performance uniformity after welding complex structures.
Special Substrate Welding Adaptation
Special welding processes are developed for difficult-to-weld substrates-"argon arc welding + preheating" for stainless steel substrates, and "laser welding +..." for high-temperature alloy substrates. "Optimization of protective gas" ensures that the weld is tight and free of cracks.

Detailed Demonstration: Witnessing Exquisite Craftsmanship in Milliseconds
Weld Nucleus
Brazed Silver Contact Assemblies. Under a metallographic microscope, a symmetrical, dense, and crack-free fusion zone should be visible, with its diameter and penetration depth fully meeting design requirements.
01
Surface Indentation
The indentation left by the welding electrode on the workpiece surface should be uniform, clear, and of consistent depth, without spatter or burns. This is a direct reflection of a stable welding process.
02
Positioning Accuracy
The positional accuracy of the weld point relative to the base reference should be controlled within extremely small tolerances, demonstrating the high precision of the automated positioning system.
03
Welding Strength
Through destructive testing (such as torque testing and tensile testing), the bond strength of the Welded Electrical Contact Parts should far exceed design requirements, and the fracture mode should be substrate fracture, not weld point detachment.
04

Materials Science and Interface Engineering: From Physical Integration to Metallurgical Innovation
| Proactive Design of Interfacial Reactions | Scientific Depth: We not only accept the inherent properties of materials, but also actively guide interfacial reactions in a favorable direction through intermediate layer design and heat treatment regulation. For example, in the welding of copper and tungsten, we introduce specific activating elements to promote mutual diffusion between the two, forming a strong and tough diffusion bonding layer, rather than a brittle direct reaction layer. |
| Gradient Design for Matching Thermal Stress | Scientific Depth: For material combinations with large differences in thermal expansion coefficients, we have developed functionally graded intermediate layer technology. Through continuous changes in composition, we achieve a smooth transition of physical properties from the AgCu Contact Assemblies for Switchgear material to the substrate, minimizing welding thermal stress while ensuring the long-term reliability of the joint under thermal cycling conditions. |
| Precise Control of Microstructure | Scientific Depth: By controlling the welding heat input and subsequent heat treatment processes, we precisely control the grain size, phase composition, and precipitate distribution in the weld zone. The optimized microstructure not only provides high strength but also ensures excellent electrical properties and resistance to softening, making the weld zone the highest-performing area in the entire Custom Electrical Contact Components system. |

contact us

Hot Tags: welded electrical contact parts, China welded electrical contact parts manufacturers, suppliers, factory, AC Resistance Welding Silver Contact, Brazed Electrical Contacts, Welding Electrical Silver Contact Tip Assembly, Spot Welding Silver Contact, Silver Contact Brazed Assemblies, Brazed Silver Contacts
You Might Also Like


Send Inquiry