


Extreme Marine and Desert Corrosion Protection for ESS Enclosures: C5-H Fluorocarbon and Cathodic Electrophoresis
Oct 20, 2026
Leave a message
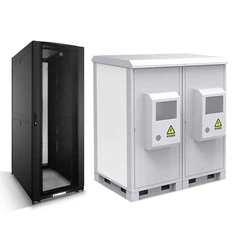
Outdoor energy storage system (ESS) enclosures installed on offshore islands and in desert photovoltaic plants face different but overlapping degradation mechanisms. Marine environments expose cabinet steel to chloride deposition, high humidity, and persistent electrolyte films, while desert installations add intense UV radiation, abrasive sand, and large temperature cycles. A qualified corrosion protection system combines substrate preparation, cathodic electrophoretic primer, a compatible PVDF fluorocarbon or weather-resistant polyester topcoat, and verified enclosure sealing.
Performance targets such as 2,000-hour neutral salt spray exposure, 3,000-hour xenon-arc weathering, coating adhesion Grade 0, and IP65/IP66 ingress protection must be supported by defined test methods and acceptance criteria.
For a C5-H Energy Storage Enclosure OEM program, coating thickness alone does not establish service life. Corrosion resistance depends on the steel substrate, pretreatment chemistry, edge coverage, coating compatibility, curing conditions, fastener interfaces, drainage design, and damage sustained during transportation and installation.

ISO 12944 C5-H Corrosion Exposure: Marine Salt and Desert Weathering
Chloride Deposition and High Humidity in Marine ESS Installations
Marine ESS cabinets are exposed to airborne salt particles that deposit on external surfaces and accumulate around seams, fasteners, hinges, and drainage features. When moisture dissolves the deposited salts, the resulting electrolyte promotes electrochemical corrosion.
Typical high-risk locations include:
Cut edges and punched holes in sheet metal
Weld seams and heat-affected zones
Door corners and overlapping flanges
Fastener interfaces and grounding points
Coating defects caused by handling or installation
For steel enclosures, corrosion can begin locally even when most of the coating remains intact. Edge preparation, weld cleaning, pretreatment coverage, and coating continuity are therefore key process controls.
Desert ESS Exposure: UV Radiation, Sand Abrasion, and Thermal Cycling
Desert installations create a different set of coating stresses. Strong solar radiation can degrade susceptible binders, causing gloss loss, color change, chalking, and embrittlement. Wind-driven sand can progressively abrade exposed surfaces, particularly around ventilation openings, lower cabinet panels, and protruding edges.
Daily temperature changes also cause differential expansion between the metal substrate, coating layers, seals, and bonded components.
| Exposure Factor | Primary Degradation Mechanism | Engineering Control |
| Marine chloride deposition | Localized corrosion and underfilm propagation | Pretreatment, primer continuity, edge coverage |
| High humidity | Electrolyte formation and corrosion acceleration | Drainage, sealed joints, compatible coating system |
| UV radiation | Binder degradation, chalking, and fading | Qualified weather-resistant topcoat |
| Wind-driven sand | Surface abrasion and coating erosion | Abrasion-resistant finish and installation protection |
| Thermal cycling | Differential expansion and seal fatigue | Coating flexibility and seal compression validation |
| Standing water | Crevice corrosion and coating damage | Drainage geometry and joint design |
ISO 12944-6 C5-H Qualification: Define the Test Before Claiming Compliance
ISO 12944 classifies protective paint systems for steel structures according to environmental corrosivity and durability considerations. The exact classification and test requirements must be checked against the applicable edition and project specification.
A C5-H designation should not be treated as an automatic guarantee that every enclosure will survive a fixed number of years in every marine or desert environment. Nor does a single salt spray result independently establish ISO 12944-6 qualification.
A project specification should define:
Substrate type and surface preparation
Primer and topcoat chemistry
Dry film thickness for each layer
Cure conditions and intercoat compatibility
Test specimen preparation and scribing requirements
Applicable cyclic or laboratory exposure methods
Acceptance criteria for blistering, rusting, cracking, and adhesion
The complete coating system should be qualified using the applicable test regime rather than relying on a supplier's generic coating datasheet.
Cathodic E-Coat Primer and PVDF Topcoat: Dual-Layer Corrosion Protection
Cathodic Electrophoresis: Uniform Primer Deposition on Complex Sheet Metal
Cathodic electrophoretic coating, commonly called e-coat, deposits a primer film through an electrically driven process. Properly designed immersion tanks allow coating material to reach many recessed and complex geometries that are difficult to cover consistently through conventional spray application.
For ESS cabinet fabrication, e-coat can provide a corrosion-resistant primer layer on suitable conductive metal substrates.
Key process variables include:
Bath solids concentration and pH
Bath temperature and electrical conductivity
Applied voltage and deposition time
Pretreatment quality
Rinse-water quality
Oven temperature and cure duration
Part orientation and drainage
The process must be validated for the actual cabinet geometry. Deep recesses, trapped air, inaccessible cavities, and shielded surfaces can affect deposition.
E-coat is not a substitute for sound weld design or surface preparation. Oil residues, weld spatter, embedded grinding debris, and poorly prepared edges can reduce adhesion or create localized corrosion initiation points.
PVDF Fluorocarbon vs. Weather-Resistant Polyester Powder: Selecting the Topcoat
PVDF fluorocarbon coatings and polyester powder coatings are not interchangeable products. They differ in binder chemistry, application methods, weathering behavior, repair procedures, and cost.
| Selection Factor | PVDF Fluorocarbon Coating | Weather-Resistant Polyester Powder |
| Application | Commonly liquid-applied systems; formulation-dependent | Electrostatic powder application |
| UV weathering | Strong performance in qualified architectural-grade formulations | Good performance with suitable exterior-grade formulations |
| Color and gloss retention | Often selected for long-term exterior appearance retention | Depends on resin grade, pigment, and exposure |
| Film formation | Requires control of wet-film application and curing | Requires control of powder deposition and thermal cure |
| Complex cabinet geometry | Spray access and film uniformity must be verified | Faraday-cage effects can limit deposition in recesses |
| Repair | Requires system-specific preparation and touch-up procedures | Local repair may not reproduce the original finish |
| Cost considerations | Often higher material and application costs | Can offer economical high-volume finishing |
The term PVDF alone does not define a coating's weathering performance. Resin content, primer compatibility, pigment system, film thickness, and cure schedule all influence the result.
Coating Adhesion Grade 0: Cross-Cut Testing and Surface Preparation
An adhesion result of Grade 0 under ISO 2409 indicates the best classification in that standard's cross-cut classification system. The result applies to the tested coating and specimen under the specified test conditions.
It does not mean the coating is immune to corrosion, impact, or long-term weathering.
To achieve repeatable adhesion, the manufacturing process should control:
Degreasing and removal of drawing oils
Abrasive or chemical surface preparation, as specified
Conversion coating where required
Rinse quality and drying
Primer-to-topcoat compatibility
Intercoat contamination
Cure profile and film thickness
The adhesion test method should be selected according to the coating system and applicable specification. Thick or elastomeric coatings may require a different evaluation method from conventional thin-film paints.
Request Free DFM Evaluation & Quote

2,000-Hour Salt Spray and 3,000-Hour Xenon Testing: Verifying Coating Performance
Neutral Salt Spray Testing Under ISO 9227: Corrosion Resistance at 2,000 Hours
Neutral salt spray (NSS) testing under ISO 9227 exposes specimens to a controlled saline atmosphere. A 2,000-hour test can be included in a project-specific coating qualification program, but it must not be interpreted as a universal requirement for all C5-H systems.
Results depend on specimen preparation, coating thickness, scribing, edge sealing, test conditions, and the acceptance criteria.
A meaningful test report should record:
Coating system and batch identification
Substrate grade and preparation method
Dry film thickness
Scribed and unscribed specimen results
Blistering, rusting, and underfilm corrosion
Adhesion before and after exposure, where specified
Photographic records and final disposition
Salt spray hours cannot be converted directly into years of outdoor service. NSS is a controlled laboratory test, not a complete simulation of offshore or desert weather.
Xenon-Arc Weathering at 3,000 Hours: UV and Moisture Resistance
Xenon-arc weathering under ISO 16474-2 can be used to evaluate changes in coating appearance and performance under specified laboratory exposure conditions.
A 3,000-hour target may be specified for an ESS cabinet coating program. However, exposure duration alone does not define qualification. Lamp filters, irradiance, black-standard temperature, moisture cycles, and specimen evaluation criteria must also be documented.
Recommended measurements include:
| Measurement | Purpose |
| Color difference, ΔE | Quantifies color change |
| Gloss retention | Measures loss of surface gloss |
| Chalking | Evaluates surface degradation |
| Cracking and flaking | Identifies coating integrity loss |
| Adhesion after exposure | Checks coating-to-substrate or intercoat bonding |
| Surface appearance | Records fading, blistering, and defects |
The specified acceptance limits should reflect the cabinet's appearance requirements, corrosion protection function, and expected maintenance strategy.
No Blistering or Delamination: Define the Acceptance Criteria
"No blistering" and "no delamination" are measurable acceptance statements only when the inspection method and test conditions are defined.
A robust qualification plan distinguishes between:
Blistering of the coating film
Rusting of the underlying substrate
Corrosion creep from a scribe
Intercoat separation
Adhesion loss
Mechanical damage caused by handling
For example, a project may require no visible blistering after the specified exposure and limit corrosion creep to a defined distance from the scribe. The actual thresholds must come from the customer specification and applicable coating standard.
Corrosion Test Matrix for C5-H ESS Cabinets
| Test | Reference Method | Purpose |
| Neutral salt spray | ISO 9227 | Evaluates behavior in controlled saline exposure |
| Cyclic corrosion testing | Project-specific applicable method | Evaluates combined corrosion stresses |
| Xenon-arc weathering | ISO 16474-2 | Evaluates weathering-related appearance and coating changes |
| Cross-cut adhesion | ISO 2409 | Classifies adhesion for suitable coating systems |
| Dry film thickness | ISO 2808 | Measures coating thickness |
| Surface preparation | ISO 8501 series, where applicable | Assesses steel surface cleanliness |
The test methods are complementary. No single test establishes the full environmental durability of an assembled cabinet.

IP65/IP66 ESS Cabinet Sealing: EPDM Gaskets and Conductive Polyurethane Foam
IP65 vs. IP66 Under IEC 60529: Dust and Water Ingress
The IP rating applies to the assembled enclosure under the specified test conditions. It cannot be established by selecting a gasket with a particular material or hardness.
Under IEC 60529:
IP6X: Dust-tight under the applicable test.
IPX5: Protection against water jets under the specified test.
IPX6: Protection against powerful water jets under the specified test.
An IP65 rating does not imply IP66 performance. Each rating requires the corresponding test, and the enclosure configuration must be representative of the final product.
The qualification should cover door closures, cable entries, ventilation interfaces, gland plates, fasteners, and other penetrations.
Dual EPDM Gaskets: Compression, Set, and Joint Continuity
EPDM gaskets are commonly used in outdoor enclosures because suitable formulations offer weathering, ozone, and moisture resistance.
For a dual-gasket arrangement, the design should define:
Gasket cross-section and dimensional tolerance
Compression range
Groove width and depth
Corner-joint design
Splice or joint location
Door-closing force
Compression-set requirements
Temperature range and chemical compatibility
Excessive compression can increase door-closing force and accelerate gasket damage. Insufficient compression can leave leakage paths at corners or along uneven cabinet flanges.
A consistent gasket profile and controlled installation process are more important than simply specifying two sealing lines.
Conductive Polyurethane Foam: Electrical Bonding and EMI Control
Conductive polyurethane foam gaskets may be used where an enclosure requires electrical continuity or electromagnetic interference (EMI) shielding across a joint.
They should not automatically be treated as substitutes for the primary environmental seal.
The design must distinguish between:
Environmental sealing
Electrical bonding
EMI shielding
Corrosion isolation
Mechanical compression support
Conductive fillers, gasket compression, surface finishes, and contact pressure affect electrical resistance. Where a grounding path is required, its resistance should be measured against the specified bonding requirement.
Door Flatness and ±0.5mm Assembly Control: Preventing Seal Leakage
Door and frame deformation can create uneven gasket compression even when the gasket itself meets its drawing.
For larger cabinet doors, dimensional control should focus on functional interfaces rather than applying one tolerance to every panel dimension.
| Critical Feature | Failure Risk | Control Method |
| Door flatness | Uneven gasket compression | Fixture inspection and dimensional measurement |
| Flange geometry | Local sealing gaps | Forming control and inspection |
| Hinge alignment | Door sag and compression variation | Assembly jig and functional test |
| Latch position | Inadequate closing force | Position measurement and closure test |
| Gasket joint | Local leakage path | Visual inspection and compression verification |
| Cable gland interface | Water ingress | Correct gland selection and enclosure testing |
A ±0.5mm tolerance may be appropriate for selected assembly features, but the actual allowable variation must be established from the cabinet's gasket design and ingress-protection test results.
Request Enclosure Design Review
Heavy-Duty ESS Enclosure Manufacturing: Sheet Metal, Welding, and Coating Control
Weld Seam Preparation: Preventing Corrosion at Fabricated Joints
Weld seams and heat-affected zones are frequent corrosion initiation points if surface preparation is incomplete.
The manufacturing sequence should account for welding distortion, spatter removal, grinding, degreasing, and pretreatment compatibility.
Recommended controls include:
Defined weld quality criteria
Removal of spatter and sharp burrs
Smooth transitions where required
Inspection of seam continuity
Drainage of enclosed or overlapping regions
Verification of coating coverage at edges and welds
Grinding should not reduce the required structural thickness or damage the surrounding sheet metal. Excessively sharp edges can also produce thinner coating films than adjacent flat surfaces.
C5-H Coating Process: Dry Film Thickness and Cure Control
Coating thickness should be specified separately for the primer and topcoat. The combined nominal thickness is not sufficient to demonstrate correct deposition or cure.
Process monitoring may include:
| Process Variable | Verification |
| Surface cleanliness | Approved visual or instrumental method |
| Pretreatment condition | Bath monitoring and process records |
| E-coat thickness | Suitable calibrated thickness gauge |
| Topcoat thickness | Measurement at defined locations |
| Oven cure | Recorded time-temperature profile |
| Adhesion | Applicable test method |
| Color and gloss | Instrumental measurement against specification |
Film thickness measurements should cover edges, recesses, corners, and other high-risk locations where practical. Measurements taken only from large flat panels may fail to detect local coating deficiencies.
Packaging and Transport: Protecting Coated Enclosures Before Installation
A qualified coating can still be damaged by abrasion, impact, or trapped moisture during shipping.
Packaging requirements should consider:
Protection of cabinet corners
Separation of coated surfaces
Moisture control during transport
Prevention of fastener abrasion
Safe lifting and handling points
Repair procedures for permitted coating damage
Any field repair system should be compatible with the original coating and documented in the product maintenance instructions.
Marine-Grade Battery Cabinet OEM: Design Validation and Quality Documentation
Environmental Qualification Before Mass Production
For C5-H Energy Storage Enclosure OEM projects, the validation plan should be agreed upon before tooling release or full-rate production.
Typical deliverables include:
Approved engineering drawings
Material and coating specifications
Process flow diagram
Welding and coating inspection plans
First-article dimensional report
Coating thickness and adhesion records
Salt spray and weathering reports, where specified
IP65/IP66 test reports, where specified
Traceability and nonconformance procedures
IATF 16949, ISO 9001, and ISO 14001 address different management-system requirements. Certification status should be stated only where valid certification applies to the actual manufacturing entity and facility. These standards do not independently certify a cabinet's corrosion resistance or IP rating.
Final Selection Matrix for Outdoor ESS Cabinets
| Application | Main Environmental Risk | Recommended Engineering Focus |
| Offshore ESS installation | Chloride deposition and persistent moisture | Coating-system qualification, edge coverage, drainage |
| Desert PV-plus-storage plant | UV exposure and sand abrasion | Weathering resistance, abrasion evaluation, seal durability |
| Coastal charging infrastructure | Salt exposure and water ingress | Corrosion protection, door seals, cable-entry validation |
| Industrial outdoor ESS | Mixed pollution and thermal cycling | Coating compatibility, joint design, maintenance access |
| High-availability ESS site | Downtime and difficult maintenance access | Replaceable seals, repair procedures, traceability |
The final specification should identify the environment, design life, maintenance interval, substrate, coating stack, film thickness, test conditions, and acceptance criteria. A coating designation alone cannot replace these requirements.
FAQ
Q: Can a C5-H ESS enclosure coating system pass 2,000 hours of neutral salt spray testing?
A: Yes, if the specified coating system passes the agreed test conditions and acceptance criteria. Results must identify the substrate, surface preparation, film thickness, specimen configuration, and applicable ISO 9227 procedure.
Q: Is PVDF better than polyester powder coating for marine-grade battery cabinets?
A: PVDF can offer strong long-term exterior weathering performance, while exterior-grade polyester powder can provide effective protection at lower application cost. Selection depends on resin formulation, corrosion-system compatibility, UV exposure, repair requirements, and qualification results.
Q: How can an outdoor ESS cabinet achieve IP65 or IP66 protection?
A: The complete enclosure must pass the applicable IEC 60529 tests. Door geometry, gasket compression, cable glands, ventilation interfaces, and panel joints must be controlled and verified in the final assembly configuration.
contact us

Send Inquiry