


Analysis of Orange Peel Defect in Powder Coating: How to Improve the Leveling and Appearance Quality of Copper Busbars at Coating?
Jun 09, 2026
Leave a message
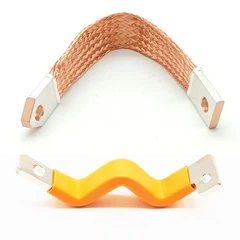
In the field of industrial coating, the appearance quality of the coating directly affects the final visual effect and protective performance of the product. Orange peel, or micro-ripples, is a common and difficult-to-overcome leveling problem during the coating process. Orange peel typically refers to a wavy structure with dimensions between 0.1mm and 10mm, appearing as wavy, alternating light and dark areas on high-gloss surfaces. This wavy structure on high-gloss surfaces causes the paint layer to appear mottled and unleveled. Especially when applying Copper Busbars at Coating, powder coatings are more difficult to remove surface defects than liquid coatings due to the lack of solvents to wet and improve film flow; therefore, controlling orange peel is particularly important.

To accurately assess leveling properties, the industry typically employs visual inspection and shape measurement methods. In visual inspection, the sample is placed under a dual-tube fluorescent lamp, and qualitative analysis is performed by observing the clarity of the reflected light. Poor flowability will result in a blurry reflection from the lamp, while high-flowability products will produce a clear reflection. Shape measurement uses a highly sensitive probe to record surface shape, quickly distinguishing between roughness caused by pinholes, craters, or contaminants and orange peel caused by poor flowability. For Powder Coated Bus Bars, surface irregularities significantly impact the overall visual appearance; even high gloss cannot mask the visual defects caused by these micro-irregularities.
The film-forming process of powder coatings includes three stages: melt agglomeration, flow film formation, and leveling. Heating at a predetermined temperature causes powder particles to melt, aggregate, and flow, ultimately chemically cross-linking to form a high-molecular-weight coating film. Key factors affecting film flow and appearance include the resin's melt viscosity, the system's surface tension, and film thickness. For Epoxy Coating Powder Busbar applications, melt viscosity depends on the curing temperature, curing speed, and heating rate. The difference between surface tension and intermolecular attraction determines the degree of leveling. If the melt viscosity is too high or the surface tension is too low, it will hinder the flow of the coating film, leading to the orange peel effect.
The inherent characteristics of powder coatings have a decisive influence on the formation of orange peel. The choice of resin molecular weight is crucial. While high molecular weight resins have good weather resistance, their high viscosity in the molten state makes leveling difficult. Furthermore, the particle size distribution of the powder directly affects leveling performance. When the proportion of powder particles larger than 75 micrometers is too high, the large particles have a long melting time, easily resulting in orange peel. In the production of Epoxy Powder Insulated Bending Copper Busbar, improper selection of leveling agents or uneven pigment dispersion in the formulation can also lead to inconsistent melting and leveling speeds, subsequently causing surface defects such as orange peel and even pinholes.

Equipment condition and process parameter control in coating production are also crucial for avoiding orange peel. Wear on the spray gun nozzle leads to poor atomization, increasing the powder thickness gradient on the workpiece surface and making leveling difficult. During the spraying of the Tinned Copper Busbar, if the hanger deforms and causes the workpiece to deflect, areas closer to the spray gun will develop ripples due to the impact of compressed air, while areas farther away will have poor leveling due to an excessively thin coating. Therefore, it is essential to regularly clean nozzle scale, replace deformed hangers promptly, and ensure the workpiece surface remains perpendicular to the spray gun to maintain a stable spraying state.
Process conditions during the curing process have a significant impact on orange peel formation. If the leveling time is too short, the resin molecules will undergo a cross-linking reaction before sufficient leveling, inhibiting the leveling effect. During the baking process of the Insulated Coating Tinned Solid Copper Busbar Connector, if the heating rate is too fast, it will increase ripples on vertical surfaces. Therefore, it is necessary to strictly control the workpiece surface temperature, appropriately slow down the heating rate in the powder melting point area, and extend the leveling time to obtain a smooth coating surface and reduce the occurrence of orange peel.
Besides coating and equipment factors, the construction environment is equally important. In Busbar Bonded Powder Coating, excessive ventilation in the powder spraying chamber leading to excessively high airflow can alter the movement of powder particles, resulting in uneven powder adhesion thickness. Furthermore, an uneven workpiece surface can hinder powder leveling. Therefore, it is necessary to properly control the ventilation in the powder spraying chamber and sand any uneven areas of the workpiece before application to comprehensively improve the leveling properties and appearance quality of the coating.

When applying Busbar Epoxy Coating, it is crucial to adhere to the powder manufacturer's recommended workpiece temperature and time. Measuring the actual temperature profile using an oven temperature tracker is the only way to ensure complete curing. Under-curing leads to performance degradation, while over-curing can cause chalking or discoloration. Optimizing the balance between spray voltage and atomizing gas pressure effectively improves coating uniformity, minimizing orange peel effect in the production of Powder Coating EV Busbars and ensuring excellent insulation and protection performance.
To achieve a perfect Busbar with Insulated Epoxy Powder Coating surface, it is essential to avoid mixing powders of the same color from different manufacturers. Differences in formulation and raw material selection can directly cause orange peel due to variations in the speed and surface tension of the mixed powders during melt flow. Furthermore, the proportion of recycled powder used should be strictly controlled to prevent cured powder particles from affecting the overall leveling effect, ensuring that the final appearance and performance of the Copper Busbars with Epoxy Powder Insulation meet optimal standards.
If you encounter surface defects such as orange peel during the coating process, or need professional technical support and solutions, please feel free to contact us. Our team of experts will provide you with customized guidance to help improve the quality of Copper Busbars with Epoxy Powder Insulation.
contact us

Send Inquiry