


314Ah & 587Ah Prismatic Energy Storage Cell Busbars: Integrated Thermal Runaway Venting & Overcurrent Capacity
Oct 15, 2026
Leave a message
A 314Ah prismatic cell delivers 314 A at 1C; a 587Ah cell delivers 587 A. At those levels, the interconnect stops behaving like a connector and starts behaving like a thermal and electromagnetic component. The production design targets that hold at 1500 V DC: conductor cross-section ≥ 400 mm² for 600 A continuous (1.5 A/mm² on C1100, 100 % IACS), busbar body ΔT < 30 K at 45 °C ambient, joint resistance < 10 µΩ per laser-welded interface, and ≥ 15 mm vertical clearance above the cell safety valve so vented electrolyte, carbonised copper and aluminium vapour cannot bridge two potential planes. Every 0.5 mm of conductor you remove to save copper mass is paid back as roughly 8–10 K of terminal temperature rise and a measurable drop in cycle life.

Why 314Ah and 587Ah Cells Invalidate Legacy 280Ah Busbar Geometry
Capacity growth in ESS has not arrived through higher voltage - it arrived through bigger electrodes and thicker stacks. The electrical consequence is a step change in continuous current, and the mechanical consequence is a step change in terminal loading and stack growth.
| Parameter | 280 Ah (legacy) | 314 Ah | 587 Ah |
| 1C continuous current | 280 A | 314 A | 587 A |
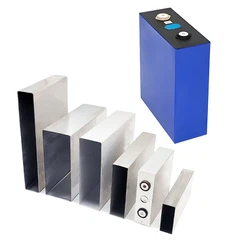
| Typical envelope (W × D × H) | 173 × 72 × 204 mm | 174 × 72 × 207 mm | ~220 × 90 × 270 mm (indicative) |
| Terminal pad/weld window | 25 × 30 mm | 30 × 38 mm | 38 × 50 mm |
| Busbar section at 1.5 A/mm² | 190 mm² | 210 mm² | 400 mm² |
| Thickness swell over 8,000 cycles | 2–3 % | 3–4 % | 4–6 % |
| Vent jet temperature at valve | 600–800 °C | 700–900 °C | 700–950 °C |
Three failure modes follow directly from this table. First, the terminal weld window grows, so a weld designed for a 25 × 30 mm pad under-fills a 38 × 50 mm pad and leaves current crowding at the pad edge - the local resistance sits where the thermocouple is attached, and the cell BMS reports a terminal fault that is actually a weld-geometry fault. Second, thicker electrodes swell more, so a rigid busbar that survived 3,000 cycles at 280 Ah shears its own weld at 6,000 cycles at 314 Ah. Third, at 587 Ah the vent mass flow roughly doubles, and a busbar routed on the valve centreline becomes a plasma bridge during propagation testing under UL 9540A or GB/T 36276.
Apollo re-runs DFM on the cell maker's terminal drawing before quoting, because pad flatness (typically ≤ 0.15 mm), pad plating (Ni 2–5 µm, or bare Al for aluminium terminals), and the cell maker's stated terminal force limit (commonly ≤ 300 N and ≤ 2 N·m) all change the process window.
Sizing the Copper: Cross-Section, Current Density and the ΔT < 30 K Budget
Current density is the only variable that simultaneously sets temperature rise, voltage drop, and copper cost. Design values below are for 600 A continuous, 200 mm unsupported span, 45 °C ambient, two joints at 10 µΩ, and an effective heat transfer coefficient of 12 W/m²K.
| Design current density | Section for 600 A | Example profile | Body loss | ΔT incl. joints | Verdict |
| 2.5 A/mm² | 240 mm² | 4 × 60 mm | 5.2 W | 40 K | Rejected at 1C duty |
| 2.0 A/mm² | 300 mm² | 5 × 60 mm | 4.1 W | 36 K | Marginal, forced air only |
| 1.5 A/mm² | 400 mm² | 5 × 80 mm | 3.1 W | 25 K | Production target |
| 1.0 A/mm² | 600 mm² | 5 × 120 mm | 2.1 W | 16 K | Sealed enclosure, no airflow |
Work the resistance directly, and the numbers are unforgiving. C1100 resistivity is 0.017241 Ω·mm²/m at 20 °C. A 400 mm², 200 mm long bar measures 8.62 µΩ; at 600 A that is 3.1 W. Two joints at 10 µΩ add 7.2 W - so the joints, not the conductor, dominate the thermal budget. Copper's temperature coefficient (α = 0.00393 K⁻¹) raises resistance by 33 % at 105 °C, which is why the 25 K figure must be validated at end-of-life contact condition rather than at T0.
| Joint method | Joint resistance | Power at 600 A | Note |
| Laser weld Cu–Cu, 2.5 mm penetration | 3–6 µΩ | 1.1–2.2 W | No filler, no aged interface |
| Molecular diffusion welding Cu–Al | 8–12 µΩ | 2.9–4.3 W | IMC controlled ≤ 3 µm |
| Resistance silver brazing (BAg-8 / BCuP-5) | 5–10 µΩ | 1.8–3.6 W | Lap ≥ 3t |
| In-die riveted Ag contact rivet | 15–25 µΩ | 5.4–9.0 W | Field-serviceable |
| Bolted M8, Sn-plated, 12 N·m | 20–40 µΩ | 7.2–14.4 W | Torque relaxes 10–15 % after 500 h at 125 °C |
Material selection follows the same arithmetic:
| Material | Conductivity | Tensile (half-hard / H04) | Softening | Typical use |
| C1100 (Cu-ETP) | 100 % IACS minimum (101 % typical) | 300–380 MPa | 180–220 °C | Main conductor, 3–5 mm |
| C2680 (CuZn30 brass) | 28 % IACS | 450–550 MPa | Not age-softened | Inserts, sensor brackets, stamped clips, nuts |
| C19400 (Cu-Fe-P) | 60–65 % IACS | 400–480 MPa | > 400 °C | Fuse links, spring terminals |
| A1060 aluminium | 61 % IACS | 80–120 MPa | - | Aluminium cell terminals, weight-critical DC links |
C2680 carries roughly a quarter of copper's conductivity, so it is never used as a current path across a 400 mm² section. It appears where mechanical strength or thread wear matters - pressed-in nut plates, Hall-sensor brackets, and stamped retaining clips at 28 % IACS on non-load paths.
Request Free DFM Evaluation & Quote
Vent-Path Clearance and 3D Formed Busbars: Stopping Arc Propagation
During thermal runaway, a prismatic cell vents through the top safety valve at 700–950 °C with jet velocities above 100 m/s. The plume carries electrolyte aerosol, carbon black, and metal vapour. Deposited on an insulation surface, that residue cuts surface resistivity by orders of magnitude; deposited across two busbars at a 1500 V DC potential difference, it initiates an arc that ignites the next cell. Propagation test data under UL 9540A and IEC 62619 show most pack-level propagation events are electrical, not purely thermal.
Design rules applied at Apollo for 314Ah and 587Ah layouts:
Standoff: ≥ 15 mm vertical clearance between the busbar underside and the valve plane, with no conductor segment crossing the valve axis within a 30 mm radius.
Offset routing: dog-leg the busbar laterally so the conductor runs over the cell shoulder, not the valve.
Local shielding: mica plate (0.5–1.0 mm) or ceramic-filled silicone-coated glass cloth over any segment that cannot be moved, rated for 800 °C short-term exposure.
Edge conditioning: burr height ≤ 0.05 mm and edge radius R ≥ 1.0 mm to suppress field concentration and corona at 1500 V DC.
Sacrificial barrier: the insulation system must survive the plume, not just the operating voltage - epoxy powder coating at 150–400 µm alone is not a vent barrier.
Clearance and creepage are then set from the system voltage with a derating factor for electrolyte contamination:
| System voltage | Clearance, IEC 60664-1 base | Applied creepage (1.5× derate) | Pack HI-POT verification |
| 1000 V DC | 5.0 mm | 8.0 mm | 3 kV AC / 60 s, ≤ 5 mA |
| 1500 V DC | 8.0 mm | 12.0 mm | 4 kV AC / 60 s, ≤ 5 mA |
| 2000 V DC | 10.0 mm | 16.0 mm | 5 kV AC / 60 s, ≤ 5 mA |
Where the pack interfaces the PCS or inverter, a laminated busbar with stray inductance < 10 nH keeps switching overshoot bounded: at SiC di/dt of 10 A/ns, 10 nH produces 100 V overshoot, about 6.7 % on a 1500 V rail. Solid single-layer bars cannot reach that figure; the laminated stack with 100–200 µm dielectric between opposing Cu layers can.
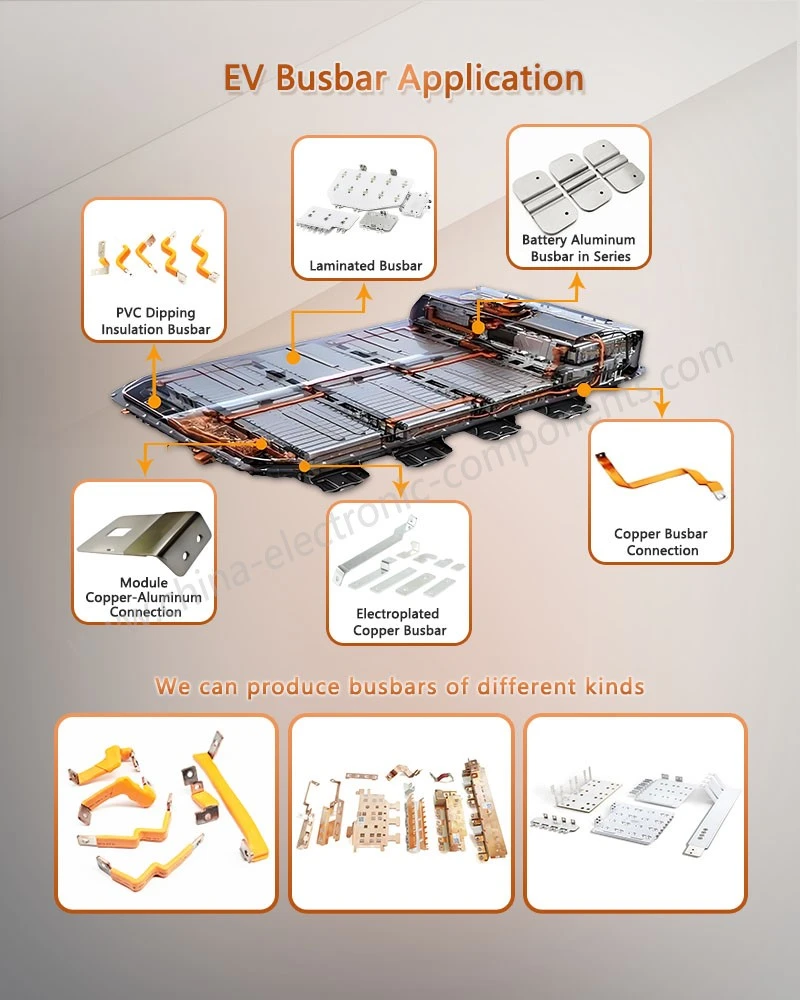
Joining: Laser Welding Cu–Cu and Cu–Al versus Resistance Silver Brazing
Thick-section copper is hostile to conduction-mode laser welding. At 1070 nm, solid copper absorbs roughly 5 % of incident energy; absorption rises sharply once the melt pool forms, which is why keyhole welding on 3–5 mm C1100 needs power density above 10⁶ W/cm² and a wobble head (0.5–1.5 mm amplitude, 100–300 Hz) to stabilise the keyhole and let hydrogen escape. Without wobble, porosity exceeds 8 % of weld area, and the joint fails ISO 13919-1 Level B.
Cu–Al joints carry a second constraint: intermetallic compounds CuAl₂ and Cu₉Al₄ are brittle and 5–10× more resistive than either parent metal. Holding the IMC layer at ≤ 3–5 µm is the difference between a joint with 60 MPa lap shear and one that cracks during module stacking.
| Process | Thickness range | Heat input / HAZ | Joint strength | Cycle time | Reference |
| Fibre laser welding, 4–6 kW, wobble | 0.5–5.0 mm Cu; 1.0–3.0 mm Al | HAZ 0.5–1.5 mm | ≥ 150 MPa Cu–Cu; ≥ 60 MPa Cu–Al | 0.5–3 s/joint | ISO 13919-1 Level B, ISO 6520-1 |
| Resistance silver brazing, BAg-8 (780 °C) or BCuP-5 (645–800 °C, self-fluxing on Cu) | 1.0–6.0 mm | Whole part annealed | ≥ 200 MPa shear | 8–20 s | AWS A5.8, ISO 17672 |
| Molecular diffusion welding Cu–Al | 0.2–3.0 mm | 400–500 °C, 20–40 MPa, no melting | IMC ≤ 3 µm, lap shear ≥ 70 MPa | 60–180 s | Internal weld spec |
| In-die riveting, Ag/Cu solid rivet | 1.0–4.0 mm | Cold | Push-out ≥ 500 N | 40–80 spm in press | Press-force monitored |
| Ultrasonic metal welding | 0.2–1.5 mm foil stacks | Cold | Foil peel per cell spec | 0.3–1.0 s | Not applicable at 4 mm |
Resistance silver brazing has one consequence that is routinely missed in RFQs: the whole part reaches brazing temperature, so cold-worked C1100 anneals. Yield strength drops from roughly 300 MPa (H04) to 60–80 MPa (annealed), and any bend or fold formed before brazing relaxes. Either form after brazing, or specify a stiffening rib and accept the softened condition.
Fault current is the last check on the joint, not on the conductor. Adiabatic heating from a cleared fault is negligible - a fuse with I²t of 8.0 × 10⁴ A²s (gR per IEC 60269) dissipates under 1 J in a 400 mm² bar. The real limits are electromagnetic: two parallel bars 30 mm apart carrying 10 kA generate about 133 N of repulsion per 200 mm span, rising to roughly 533 N at 20 kA. Support spacing and fold geometry, not section area, decide whether the busbar survives a short circuit.
Download Busbar Design Specification
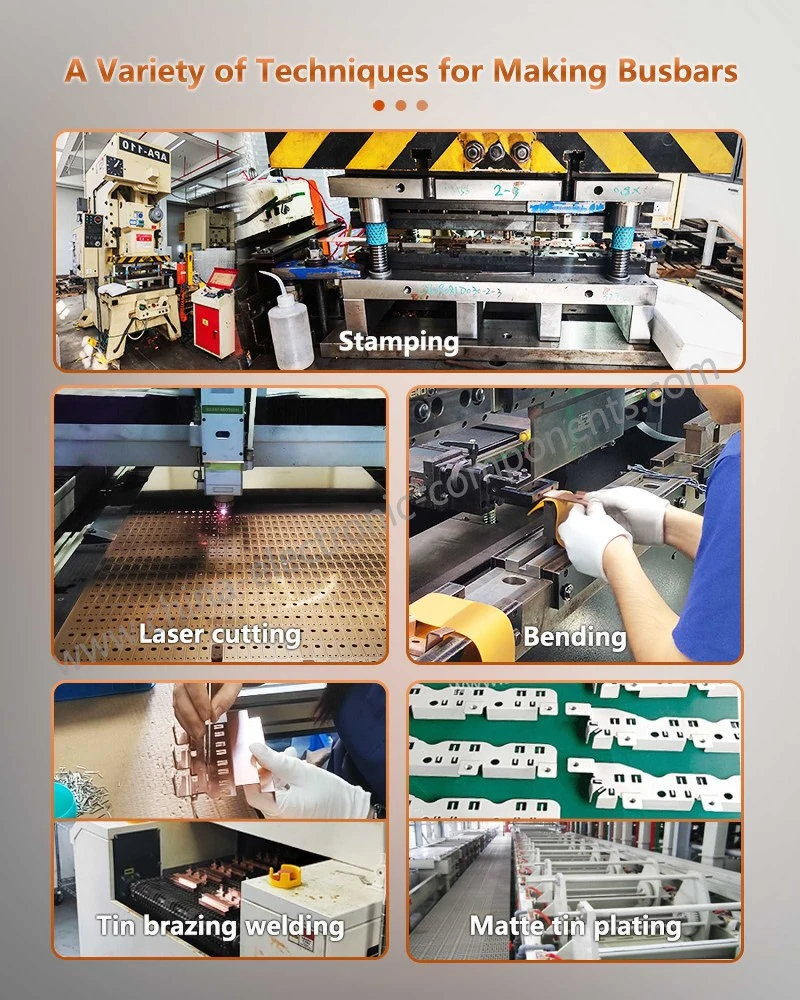
Swelling Compensation: U-Folds and Ω-Folds for 8,000 Cycles
A 314Ah cell grows 3–4 % in thickness across its cycle life. On a 174 mm-wide cell, that is 5–7 mm of stack movement; across a 20-cell module the end-plate displacement reaches double digits, and every cell-to-cell busbar sees the differential. A rigid bar converts that displacement into terminal shear.
| Fold type | Axial displacement absorbed | Reaction force at max travel | Bend radius | Application |
| U-fold, single | ± 1.5 mm | 35 N | R ≥ 1.5t | Cell-to-cell within a module |
| Ω-fold, double | ± 3.0 mm | 55 N | R ≥ 1.5t | Module-to-module, end plates |
| S-offset / dog-leg | ± 0.8 mm | 90 N | R ≥ 2t | Vent-clearance routing |
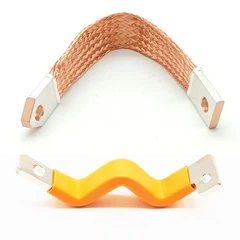
| Braided copper flexible | ± 6.0 mm | 20 N | n/a | HV junction, service loops (resistance +30 % vs solid) |
Fold design details that decide fatigue life: use soft-temper C1100 (R220) in the fold zone so the strain distributes instead of concentrating; orient the rolling grain perpendicular to the bend line; hold bend radius ≥ 1.5t to avoid grain-boundary cracking; and verify grain size to ASTM E112 after any annealing step. The target is 3,000 displacement cycles with resistance drift ≤ 10 %, then vibration per UN 38.3 T3 and SAE J2380 random profiles (10–2000 Hz, three axes), with the busbar first natural frequency either above 100 Hz or deliberately decoupled from the cell stack mode.
Insulation System: Epoxy Powder Coating versus Heat Shrink and Overmolding
| Method | Thickness | Dielectric strength | Continuous rating | Flammability | Dominant failure mode |
| Epoxy powder coating, electrostatic/fluidised bed | 150–400 µm | > 15 kV/mm (typ. 20–30 kV/mm) | 130 °C RTI | UL 94 V-0 | Pinhole at a burr, edge chipping |
| PET heat shrink sleeve | 200–500 µm | 15–20 kV/mm | 125 °C | UL 94 V-0 / VW-1 | Sliding, trapped air pockets |
| PVC dip coating | 300–800 µm | 10–15 kV/mm | 90 °C | UL 94 V-0 | Plasticiser migration, cracking |
| PA66 / PPS overmolding | 0.8–2.0 mm | 15–25 kV/mm | 140 °C | UL 94 V-0 | Tooling cost, sink marks |
| Mica + ceramic silicone shield (vent zone) | 0.5–1.5 mm | > 20 kV/mm | 800 °C short-term | Non-combustible | Mechanical damage |
At 300 µm, an epoxy coating rated at 20 kV/mm gives 6 kV of dielectric headroom against a 4 kV HI-POT - a 1.5× margin that collapses to 1.1× at 150 µm, which is why Apollo specifies 150 µm as a floor and 400 µm as the vent-zone target. Partial discharge inception voltage is checked on sample parts; EN 45545-2 (R22/R23) applies where the pack enters rail-adjacent installations, and ISO 14001 governs the coating line's VOC and powder-recovery handling.
From DFM to PPAP Level 3: Tooling, Inspection and Traceability
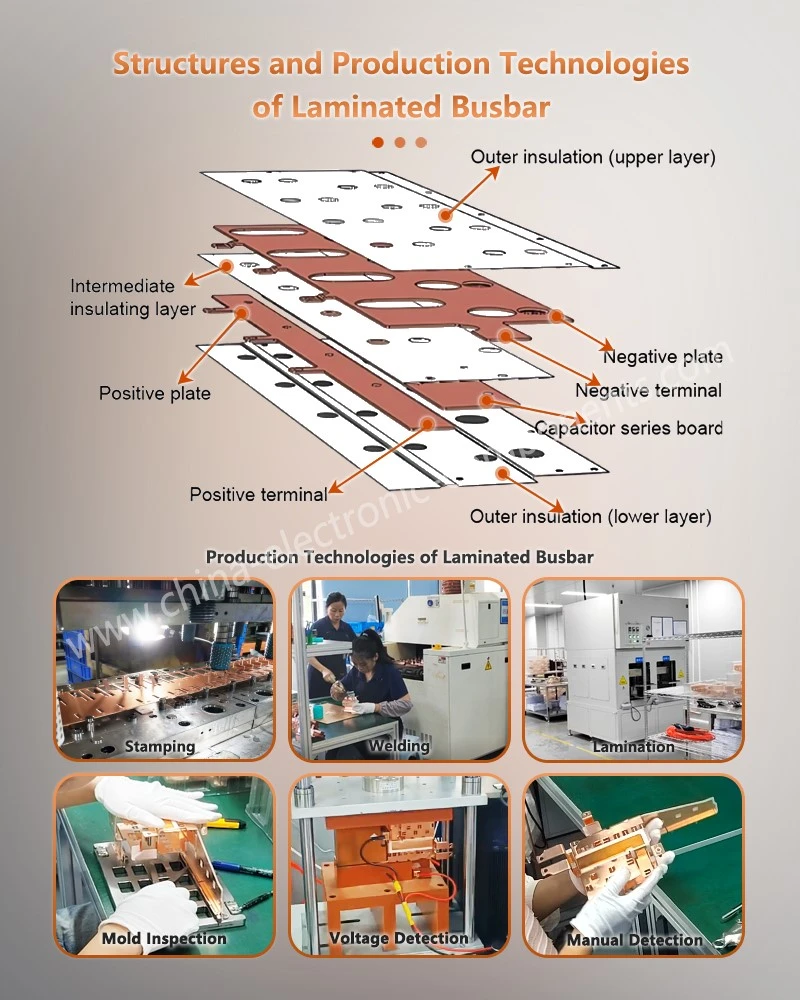
Stamping 4 mm C1100 in a progressive die is a tonnage and burr-control exercise, not a forming exercise. Blanking force for a 5 × 80 mm profile at 200 MPa shear strength is about 170 kN before stripping and drawing loads, so production runs sit on 250–400 t servo presses at 40–60 spm with 8–14 stations, in-die tapping and in-die riveting where the design calls for contact rivets.
| Characteristic | Method/gauge | Frequency | Acceptance |
| Terminal pitch, hole diameter, slot width | CMM, 2.4 µm + L/300 µm | First/last + 5 pcs/lot | ± 0.01 mm, Cpk ≥ 1.67 |
| Burr height | Digital microscope / CCD vision | 100 % | ≤ 0.05 mm |
| Weld penetration and porosity | Metallographic cross-section | 1/500 + every setup | ≥ 1.5 mm penetration on 4 mm stack, ≤ 5 % porosity |
| Joint resistance | 4-wire micro-ohmmeter at 100 A | 100 % | ≤ 10 µΩ |
| Coating thickness | Eddy-current gauge, 5 points/part | AQL 0.65 per ISO 2859-1 | 150–400 µm, Cpk ≥ 1.33 |
| Dielectric | AC HI-POT | 100 % | 4 kV AC / 60 s, ≤ 5 mA |
| Burst pressure (liquid-cooled variants) | Hydrostatic rig | 1/500 | 8 bar / 60 s, no rupture |
| Thermal cycling | Chamber −40 / +85 °C | 3 pcs/lot | 300 cycles, ΔR ≤ 10 % |
| Salt spray | ISO 9227 NSS | Quarterly | 480 h, no base-metal corrosion |
| Material verification | Spectrometer + mill certificate | Per heat lot | Cu ≥ 99.90 %, ≥ 100 % IACS |
Documentation ships under IATF 16949 with PPAP Level 3, IMDS entry, RoHS and REACH declarations, and full heat-lot traceability from mill certificate to finished pallet.
Frequently Asked Questions
What is the T1 sample lead time for a custom 314Ah prismatic cell busbar, and is PPAP Level 3 included?
T1 stamped samples ship 15–20 working days after DFM sign-off on soft tooling; a hard progressive die takes 35–45 days. PPAP Level 3 ships with the first production lot - dimensional reports, CMM data, weld cross-sections, HI-POT and salt spray records.
How do you verify coating thickness and dielectric strength on epoxy powder-coated ESS busbars?
Thickness is measured at five points per part by eddy-current gauge: 150–400 µm, Cpk ≥ 1.33. Every part passes 4 kV AC HI-POT for 60 s, leakage under 5 mA, plus per-lot 6 kV DC surge and 480 h ISO 9227 salt spray.
What tooling life can we expect on a 4 mm C1100 progressive die, and who owns the tool?
A 4 mm C1100 progressive die with powder-metallurgy inserts is rated for 1.5–2 million strokes, with regrinds every 150,000. Tooling ownership transfers to you on final payment; Apollo stores and maintains it free for five years.
contact us
Send Inquiry