



Fuse Cap Contact Soldering
Products Description

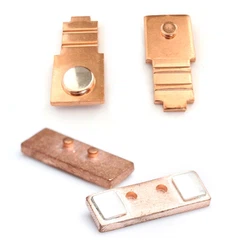
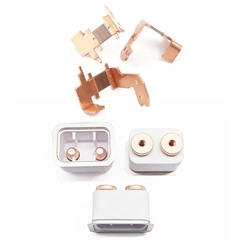
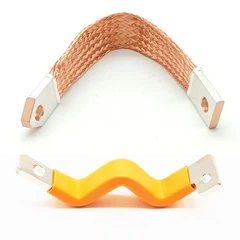
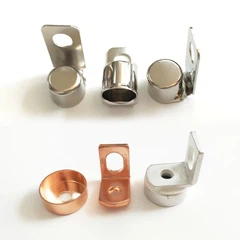
Fuse Cap Contact Soldering is a conductive connector installed at both ends of a high-voltage fuse in new energy applications. It forms a stable mechanical and electrical connection with the fuse element or electrical contact structure through welding. It not only performs the function of circuit switching but also undertakes critical tasks such as heat conduction and improving short-circuit protection triggering efficiency.
The design logic of this component focuses on conductivity reliability, safety redundancy, heat resistance, and mechanical stability. It is suitable for the main circuit protection of power battery packs, high-voltage distribution boxes, high-voltage relay systems, electric drive controllers, and energy storage power modules.
Manufacturing Advantages and Technological Features: Mastering the Art of Connection in the Microscopic World
Core Technology – Controlled Atmosphere Welding
We employ high-frequency induction welding or laser welding technology under nitrogen protection. Welding in an oxygen-free environment eliminates weld oxidation and porosity. We use PLC to precisely control heating temperature, time, and curves, ensuring uniform weld microstructure, fine grains, and a perfect balance of strength and toughness.
Key Technology – Precision Forming and Pre-treatment
The Fuse Cap and Contact Joined by Tin Brazing and the cap body are formed using high-precision continuous die stamping, ensuring dimensional accuracy and consistency. Before welding, all components undergo ultrasonic cleaning and plasma surface treatment to remove oil and activate the surface, creating optimal conditions for perfect solder wetting and atomic diffusion.
Key Quality Control – Non-Destructive Testing of Weld Joints
We have introduced industrial X-ray inspection equipment to perform 100% non-destructive testing on every weld joint. Under X-ray imaging, any tiny pores, cracks, or incomplete welds will be clearly visible. This is the source of our confidence in promising you "zero-defect" solder joints.

Materials Science Depth: Synergistic Optimization of Microscopic Interfaces and Performance
| Interface Engineering Revolution | The conductivity of traditional contact cap assemblies relies primarily on the physical contact of the contact surfaces, but this Fuse Cap and Contact Resistance welding is highly susceptible to change during vibration and thermal cycling. Our product utilizes innovative interface engineering to create a stable intermetallic compound interface between the contact cap and the fuse terminal. This interface is not a simple "contact," but rather a stable chemical bond formed at the microscopic level through a precisely controlled heat treatment process, ensuring long-term stability of contact resistance and avoiding the contact resistance fluctuation problems common in traditional designs. |
| Stress-Free Conductive Path Design | In high-voltage systems, stress concentration is a major cause of connection failure. Our Fuse Cap and Contact Tin welding, through innovative structural design, avoid stress concentration points, ensuring the stability of the conductive path during long-term vibration and thermal cycling. This design is not simply about "increasing thickness," but rather about proactively designing the microstructure to ensure the uniformity and reliability of the conductive path. |
| Deep Synergy Between Thermal Management and Conductivity | Copper has good conductivity but a high coefficient of thermal expansion, while aluminum has slightly lower conductivity but a low coefficient of thermal expansion. Our Copper Contact for Bolted Tag Fuse achieves a deep synergy between thermal management and electrical conductivity through an innovative bimetallic interface design. This synergy is not a simple "material combination," but rather a process of micro-interface engineering that ensures stable electrical conductivity during thermal changes, avoiding performance fluctuations caused by temperature variations. |

Detailed Showcase: Excellence Stems from a Dedicated Focus on Key Aspects
Microscopic Perfection of the Weld Interface
Metallographic analysis reveals a uniform and dense intermetallic compound layer at the weld interface, with a thickness controlled within the ideal range of 1-3 μm, free from defects such as porosity and cracks.
Precise Control of Coating Quality
X-ray fluorescence thickness gauges are used to perform 100% inspection of the coating thickness, ensuring that the thickness tolerance is controlled within ±0.5 μm, laying the foundation for consistent weld quality.
The Ultimate Pursuit of Dimensional Accuracy
The tolerance of key installation dimensions is controlled within ±0.05 mm, providing a precise positioning benchmark for automated assembly, significantly improving production efficiency and quality consistency.

contact us

Hot Tags: fuse cap contact soldering, China fuse cap contact soldering manufacturers, suppliers, factory, End Cap and Terminal, Fuse Contact Knife Cap, End Cap and Contact, Fuse Cap Contact Resistance Welding, Outer Cap and Contact, Copper Cap Contact For Vehicle Fuse
You Might Also Like


Send Inquiry